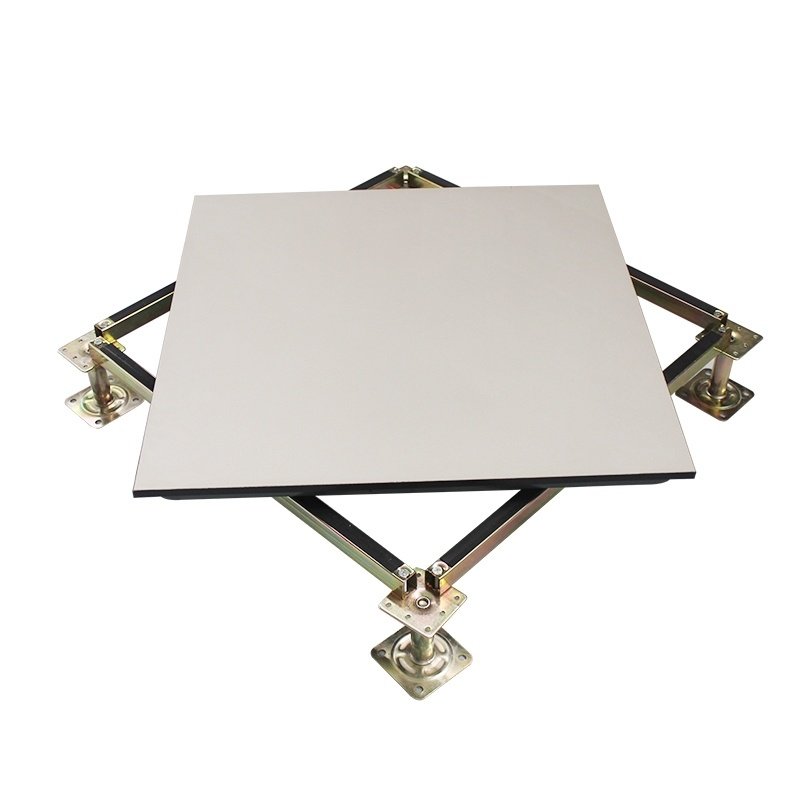
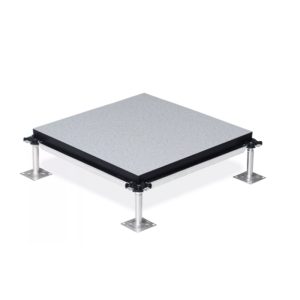
The Calcium Sulphate Raised Access Floor is a high-performance anti-static raised flooring system designed for data centers, server rooms, laboratories, and other mission-critical environments. Manufactured in a standard 600 × 600 mm panel size, each panel features a high-density calcium sulphate core, offering exceptional load-bearing capacity, dimensional stability, and long-term durability.
Panel thickness can be customized to meet different static and rolling load requirements. All panels are equipped with ABS edge protection, effectively reducing damage during installation and daily maintenance. The bottom layer is reinforced with a galvanized steel sheet, securely bonded to the core to enhance overall strength and impact resistance.
Multiple anti-static surface finishes are available, including high wear-resistant HPL, permanent anti-static PVC, and anti-static ceramic tile, ensuring excellent ESD control while maintaining a clean and professional appearance.
As one of the most advanced raised floor systems, calcium sulphate access flooring delivers superior fire resistance, thermal insulation, sound insulation, acoustic comfort, and eco-friendly performance, making it an ideal solution for high-standard technical spaces.
Applications of Calcium Sulphate Raised Floor
This anti-static calcium sulphate raised floor system is widely used in environments requiring strict ESD protection and structural performance, such as:
Data centers and server rooms
Computer rooms and IT infrastructure facilities
Laboratories and research centers
Telecommunications rooms and operator core sites
Semiconductor manufacturing and R&D facilities
PCB production lines and electronics factories
Clean rooms and precision assembly workshops
Key Features & Advantages
High load capacity raised floor with reinforced calcium sulphate core