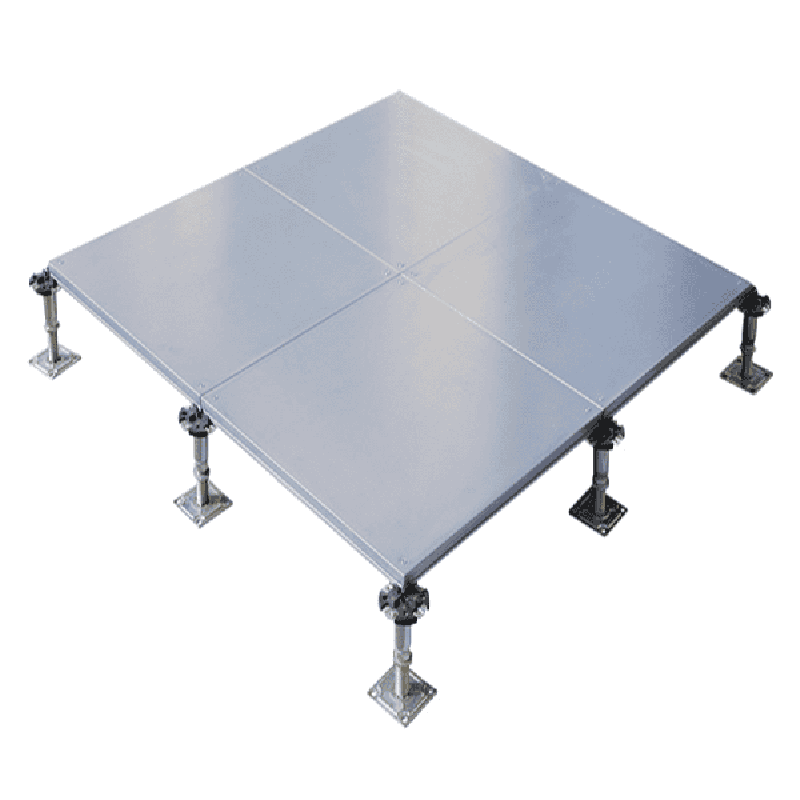
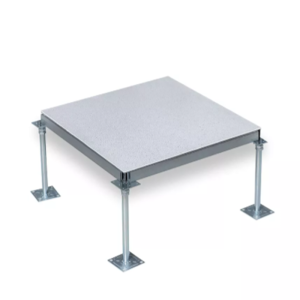
The six-sided steel-encased calcium sulphate raised floor is fully wrapped with hot-dip galvanized steel sheets. The top and bottom steel panels are firmly bonded through pressing and riveting processes, enclosing a high-strength calcium sulphate core. With a standard size of 600 × 600 mm, the panel features an integrated structure that delivers both strength and long-term stability.
Applications
This product is suitable for office buildings, telecommunications rooms, power plants, factory cleanrooms, and various spaces with high requirements for cable management. The surface is commonly finished with square carpet tiles, combining functional performance with aesthetic appeal.
Product Features
Excellent fire resistance performance
Recyclable materials, environmentally friendly
Outstanding load-bearing capacity with a stable structure
Fully enclosed steel casing with superior sealing
Enhanced water and moisture resistance
High dimensional accuracy for easy installation and system compatibility
Product Advantages
Among all raised floor systems, calcium sulphate raised floors stand out for their exceptional fire performance, offering significant value in both functionality and safety. The calcium sulphate core material is inherently non-combustible.
Calcium sulphate raised floors perform well in mildly humid environments, are easier to maintain and clean, and provide a much longer service life than traditional particleboard raised floors. Manufactured with high-quality raw materials, the high-strength calcium sulphate core combined with premium steel-encased surface and base layers ensures excellent durability, structural stability, and long-term reliability.