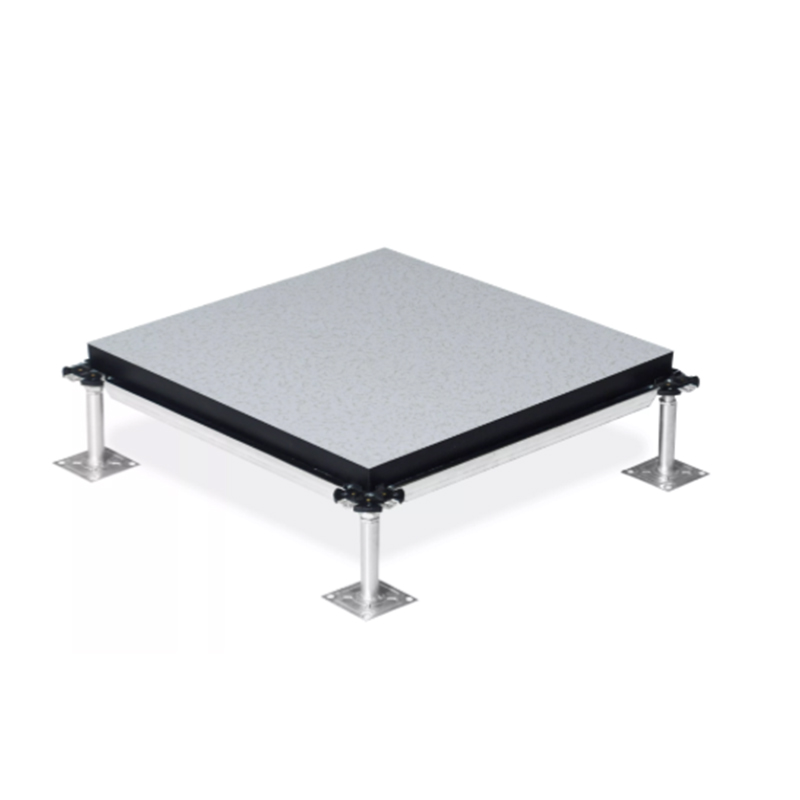
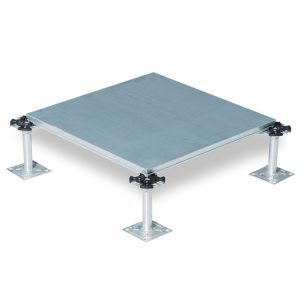
The Calcium Sulphate Raised Access Floor System consists of standard 600 × 600 mm panels with a high-density calcium sulphate mineral core, delivering excellent strength, stability, and long-term performance. Panel thickness can be customized to meet different load-bearing requirements, making the system suitable for a wide range of technical environments.
Each panel is fully protected with ABS edge trimming, ensuring optimal edge protection during installation, relocation, and daily use. The underside of the panel is reinforced with a galvanized steel sheet, firmly bonded to the core through an advanced adhesive process to enhance structural integrity.
The surface finish is available in multiple anti-static options, including high wear-resistant HPL, permanent anti-static PVC, and anti-static ceramic tiles, providing reliable ESD control and durable surface performance.
As a premium solution among raised access floor systems, calcium sulphate raised flooring is ideal for applications requiring high mechanical strength, Class A fire resistance, thermal insulation, acoustic comfort, and environmentally friendly materials with no harmful emissions.
Applications
This anti-static calcium sulphate raised floor is widely used in environments with strict electrostatic discharge (ESD) control requirements, including:
Laboratories and research facilities
Data centers and server rooms
Telecom training rooms and classrooms
Computer rooms and IT infrastructure facilities
Communication base stations and operator core rooms
Semiconductor R&D and manufacturing workshops
PCB production lines
Precision electronics assembly plants
Key Features
High load-bearing structure with excellent load capacity
Outstanding mechanical resistance and stable panel construction
Effective sound insulation, providing superior acoustic comfort
Thermal insulation and moisture resistance for improved environmental adaptability
Class A fire-rated raised floor system with high fire resistance
High-quality surface finishes with multiple anti-static options
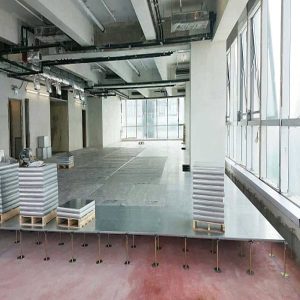
Easy installation, relocation, and maintenance, supporting flexible floor planning
Multiple surface and application configurations to meet diverse project needs