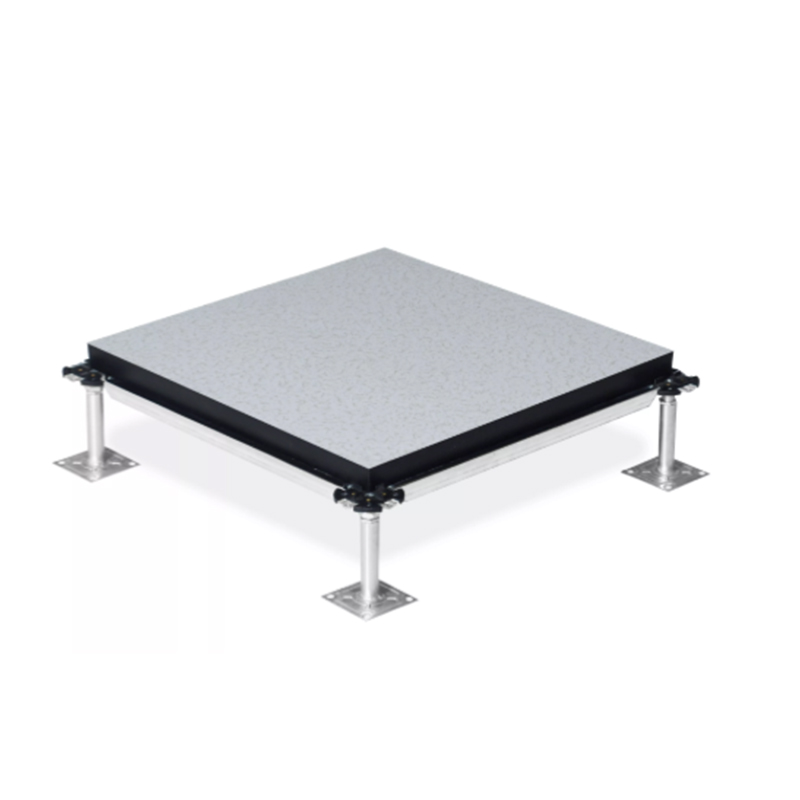
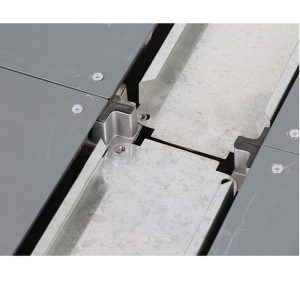
The calcium sulphate raised access floor system is composed of 600 × 600 mm panels with a high-density calcium sulphate mineral core. Panel thickness can be customized according to specific load-bearing requirements. Each panel edge is protected with ABS edge banding to ensure maximum edge durability and protection.
The bottom layer is made of galvanized steel, securely bonded to the upper panel to enhance structural strength. A wide range of anti-static surface finishes is available, including super wear-resistant HPL, permanent anti-static PVC, and anti-static ceramic tiles.
Calcium sulphate raised floors are widely recognized as one of the highest-performing solutions in this product category. They are particularly suitable for high-performance flooring applications that require excellent mechanical strength, fire resistance, thermal insulation, sound insulation, and zero harmful emissions.
Applications
This flooring system is ideal for professional environments with strict anti-static requirements, including:
Laboratories
Data centers
Server rooms
Telecommunication training rooms
Computer rooms
Communication base stations and operator core rooms
Electronic chip R&D and manufacturing workshops
PCB production lines
Precision electronic assembly facilities
Product Features
High load-bearing structural design with outstanding strength
Excellent mechanical performance and impact resistance
Superior sound insulation for enhanced acoustic comfort
Good thermal insulation with moisture resistance
High fire resistance with Class A fire rating
Multiple surface finish options with long-lasting quality
Easy installation, relocation, and maintenance
Supports various coatings and applications with strong adaptability