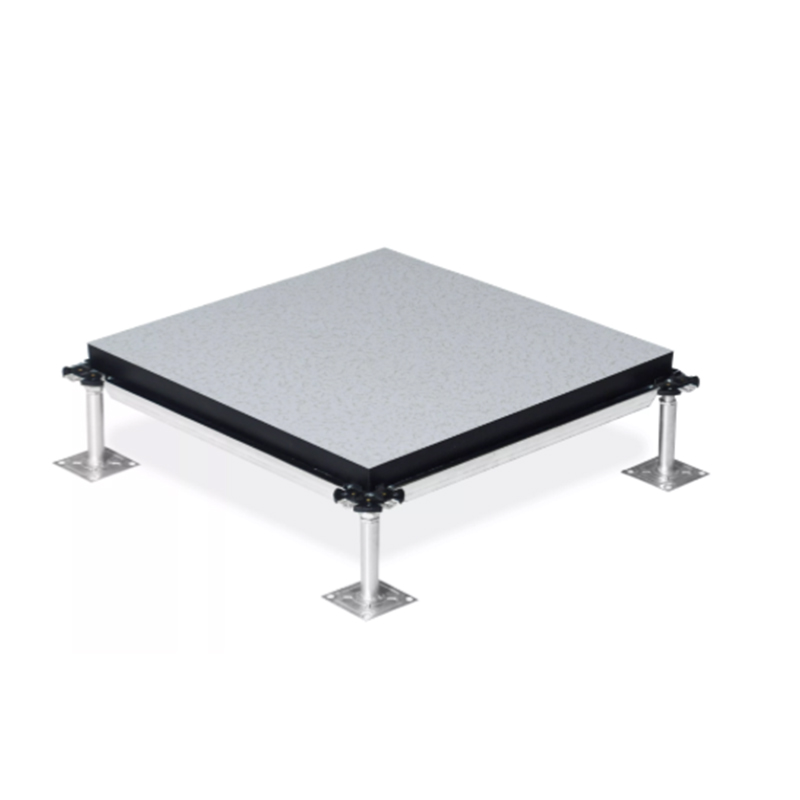
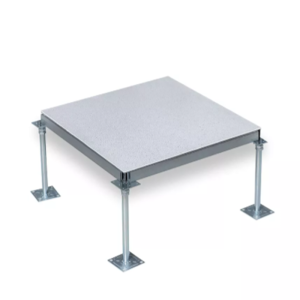
The Calcium Sulphate Raised Floor System consists of 600 × 600 mm panels manufactured with a high-density calcium sulphate (mineral) core. Panel thickness can be selected according to the required load performance. Each panel edge is protected with ABS edging, providing maximum impact resistance and long-term durability.
The underside of the panel is bonded with galvanized steel and coated, ensuring excellent structural stability. A wide range of anti-static surface finishes is available, including high-wear-resistant HPL, permanent anti-static PVC, and anti-static ceramic tiles.
Calcium sulphate raised floors are widely regarded as one of the highest-performance access floor solutions, ideal for environments requiring high mechanical strength, fire resistance, thermal insulation, acoustic performance, and zero emissions.
Applications
The calcium sulphate raised floor system is suitable for environments with strict anti-static and performance requirements, including:
Laboratories
Data centers
Server rooms
Telecommunication classrooms
Computer rooms
Telecom base stations and core network rooms
Semiconductor R&D and manufacturing facilities
PCB production lines
Precision electronic assembly workshops
Key Features & Benefits
High load-bearing structure with excellent load capacity
Outstanding mechanical resistance and dimensional stability
Superior sound insulation, providing high acoustic comfort
Thermal insulation and moisture resistance
Excellent fire performance, classified as A-grade non-combustible
Unlimited premium surface finish options
Easy installation, with simple relocation and maintenance
Multiple coatings and application solutions for different usage requirements